


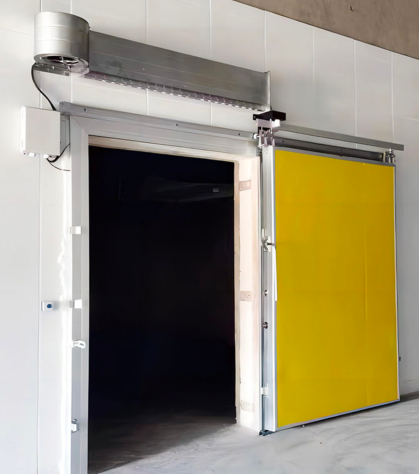


Pharmaceutical Cold Chain Storage Raises Higher Standards for Insulation panels, Condensing units, Condensers.
As a core carrier for the safe storage of vaccines, pharmaceuticals, and biological products, pharmaceutical cold chain cold storage is subject to far stricter industry standards than ordinary fresh-keeping cold storage. It must fully comply with GSP specifications and national cold storage design codes, featuring constant temperature stability, zero temperature deviation, and safe and efficient operation. The three key components— insulation panels, condensingunits, and condensers—determine the compliance level, operational stability, and long-term safety of pharmaceutical cold storage.
1.Insulation PanelsUltra-Low Thermal Conductivity & Full-Sealed Fireproof Insulation Performance
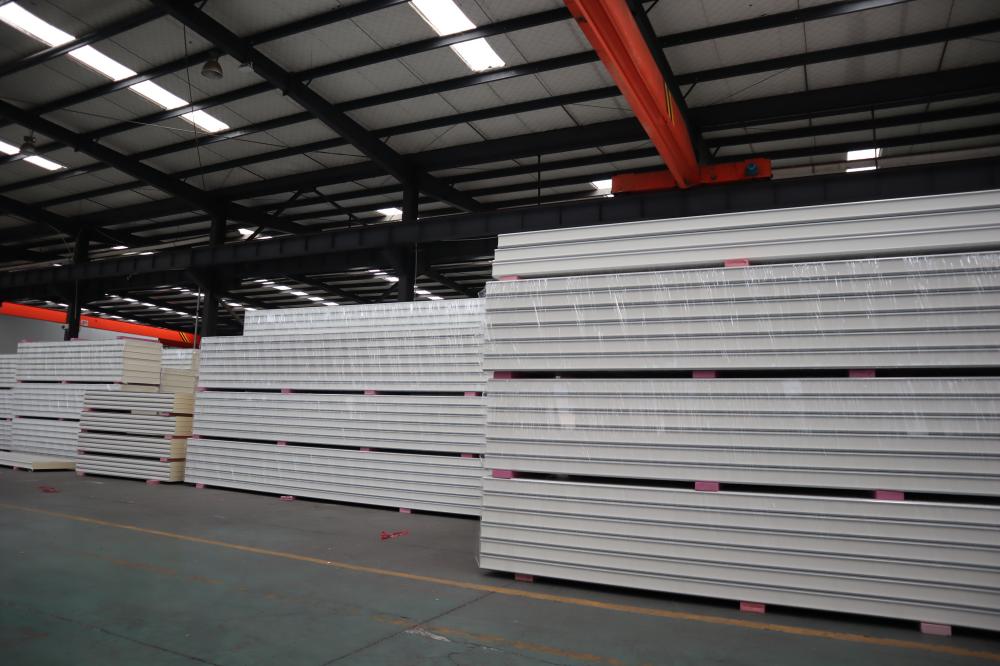
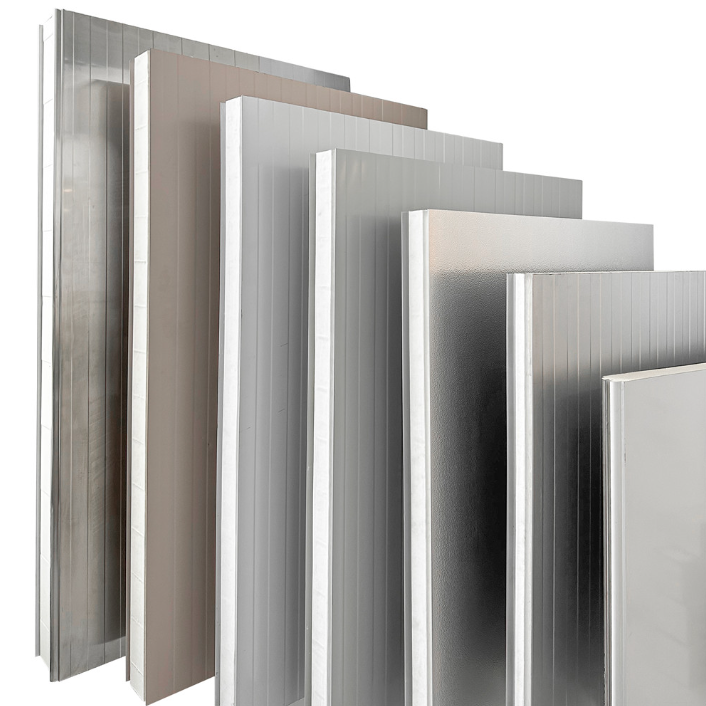
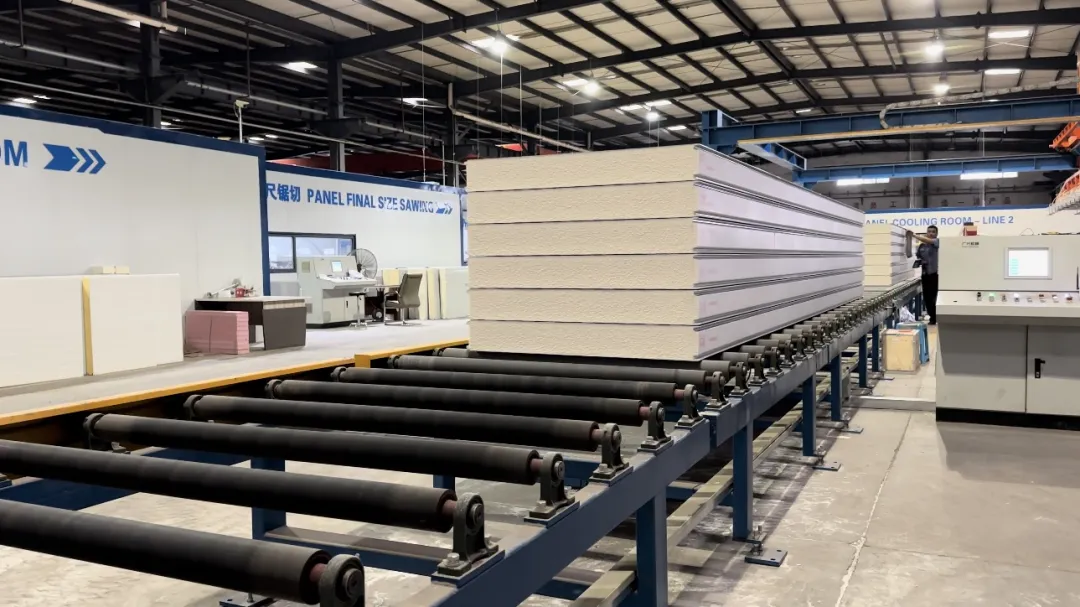
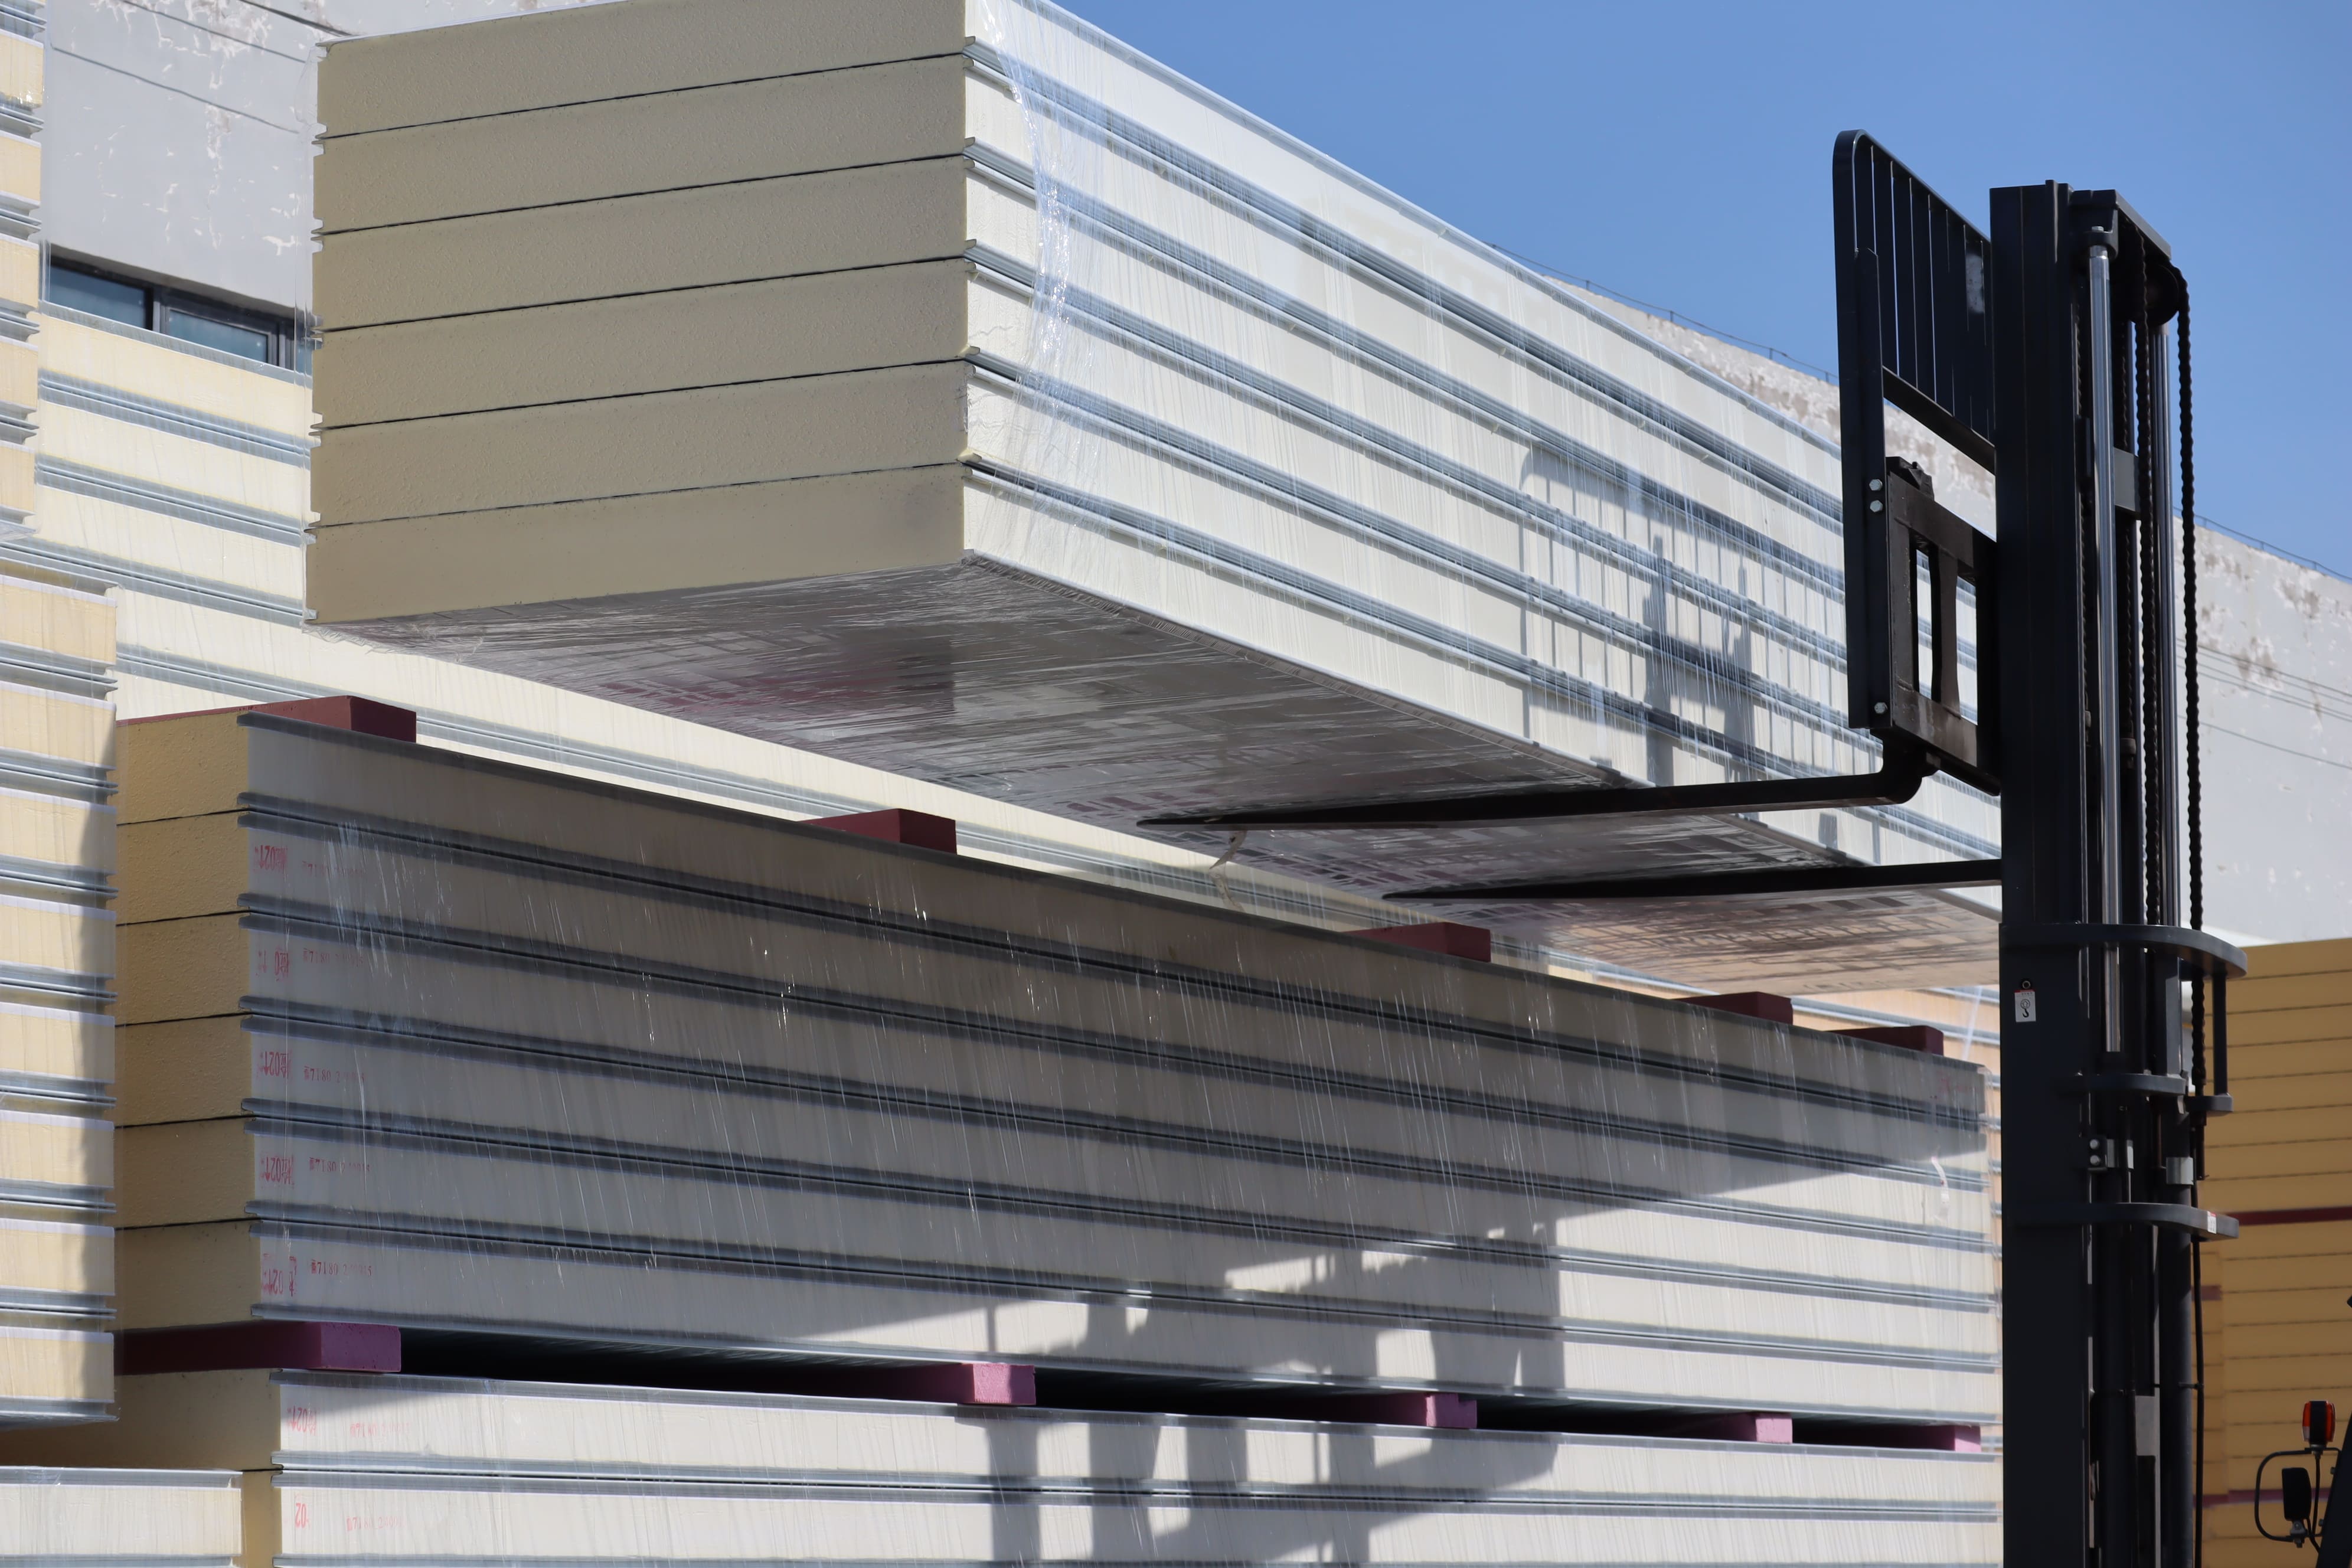
Different from ordinary cold storage panels that only pursue basic heat preservation, pharmaceutical cold storage insulation panels take constant temperature locking, low heat leakage, fire safety, and corrosion resistance as the core standards. Qualified pharmaceutical-grade insulation panels adopt high-density polyurethane (PIR/PUR) materials, with a thermal conductivity controlled below 0.024W/(m·K), which effectively blocks external heat infiltration and avoids frequent temperature fluctuations inside the Cold Room.
In terms of specification matching, 2–8°C pharmaceutical constant-temperature cold rooms adopt panels with a thickness of no less than 100mm, while low-temperature pharmaceutical freezing cold room require 150mm thick panels with a material density of more than 40kg/m³. All panels reach B1-level flame retardant standard, featuring integral seamless splicing and double-layer door sealing design. This eliminates cold leakage gaps, ensures long-term stable insulation effect.
 |  |
2.CondensingUnits: High Stability & Redundant Backup for 24/7 Continuous Operation
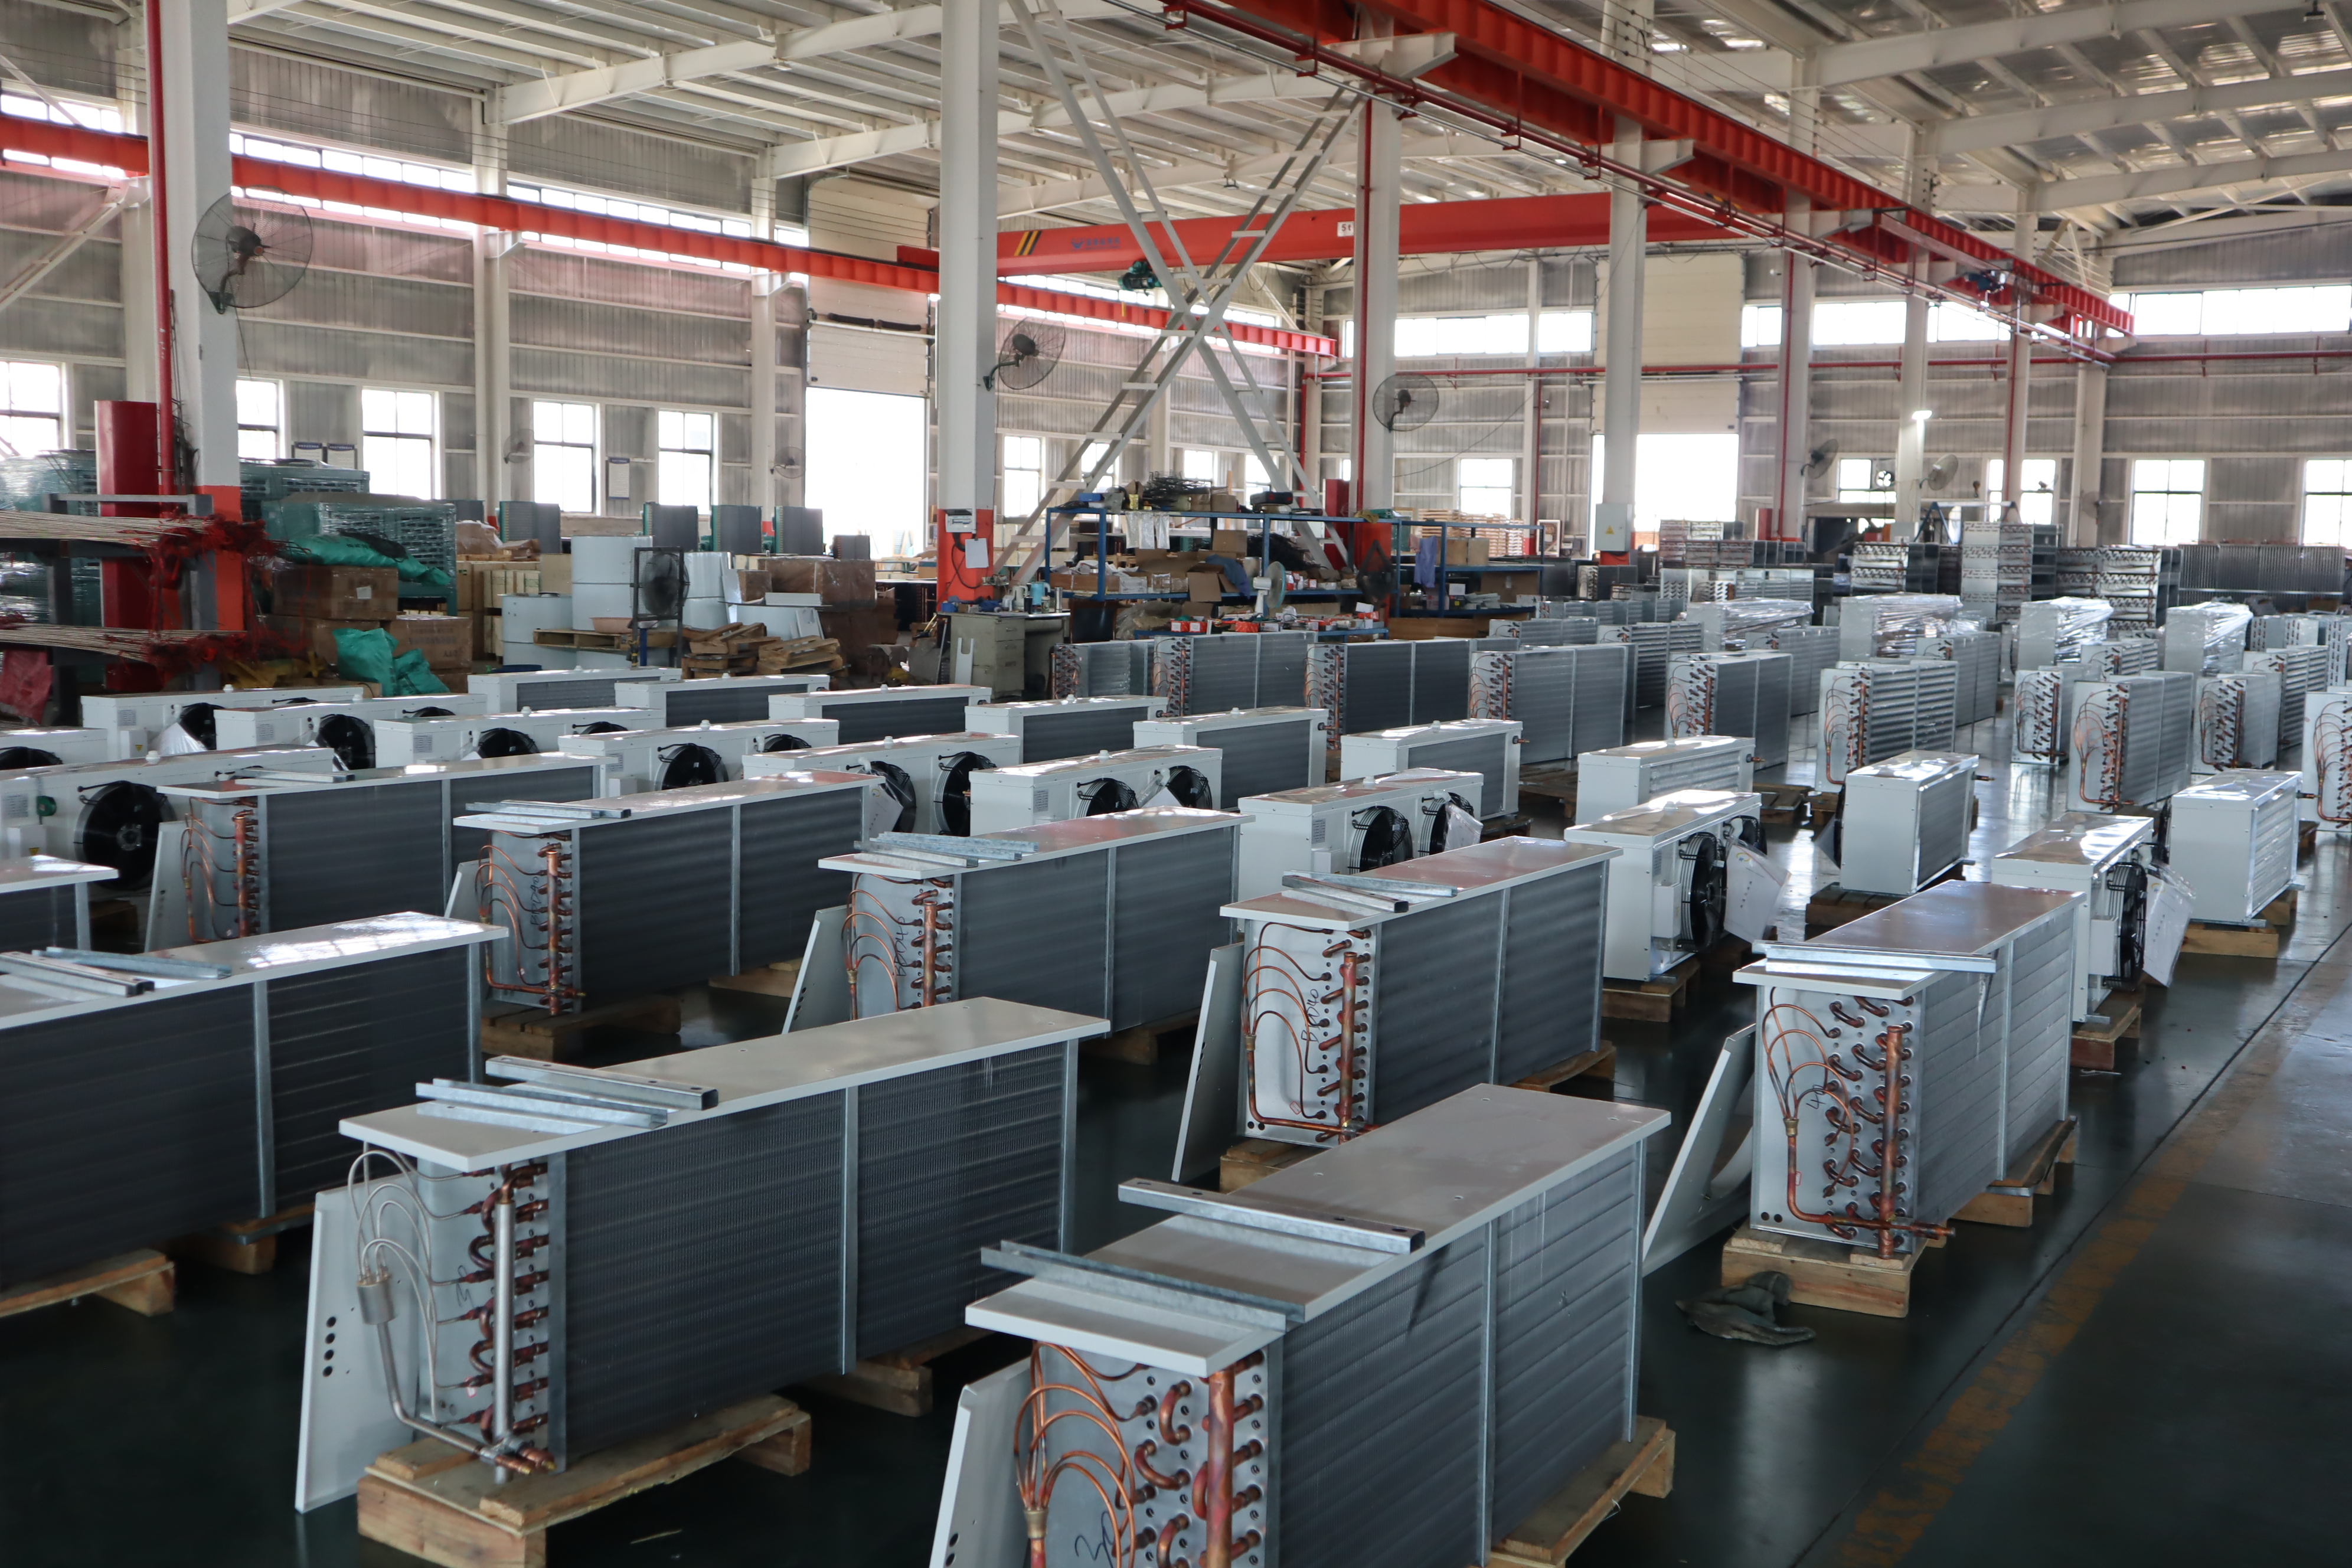
Pharmaceutical storage has zero tolerance for temperature interruption. Once the equipment shuts down abnormally, it will lead to pharmaceutical failure and huge losses. Therefore, condensingunits for pharmaceutical cold chains abandon conventional single-unit configuration and focus on continuous operation stability, precise temperature control, and emergency backup capability.
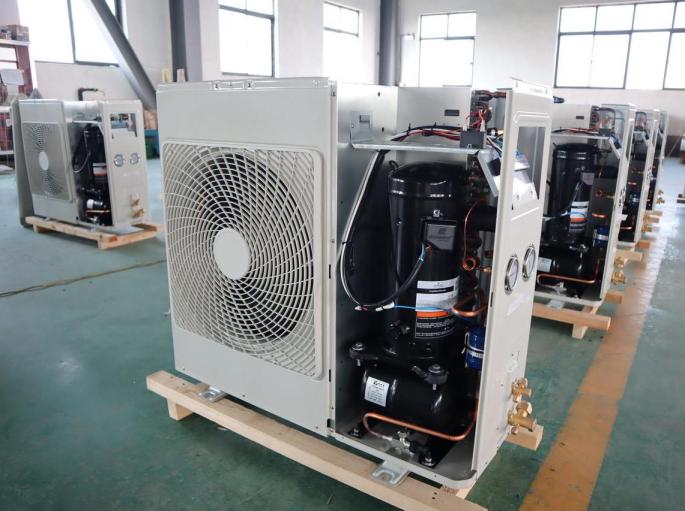
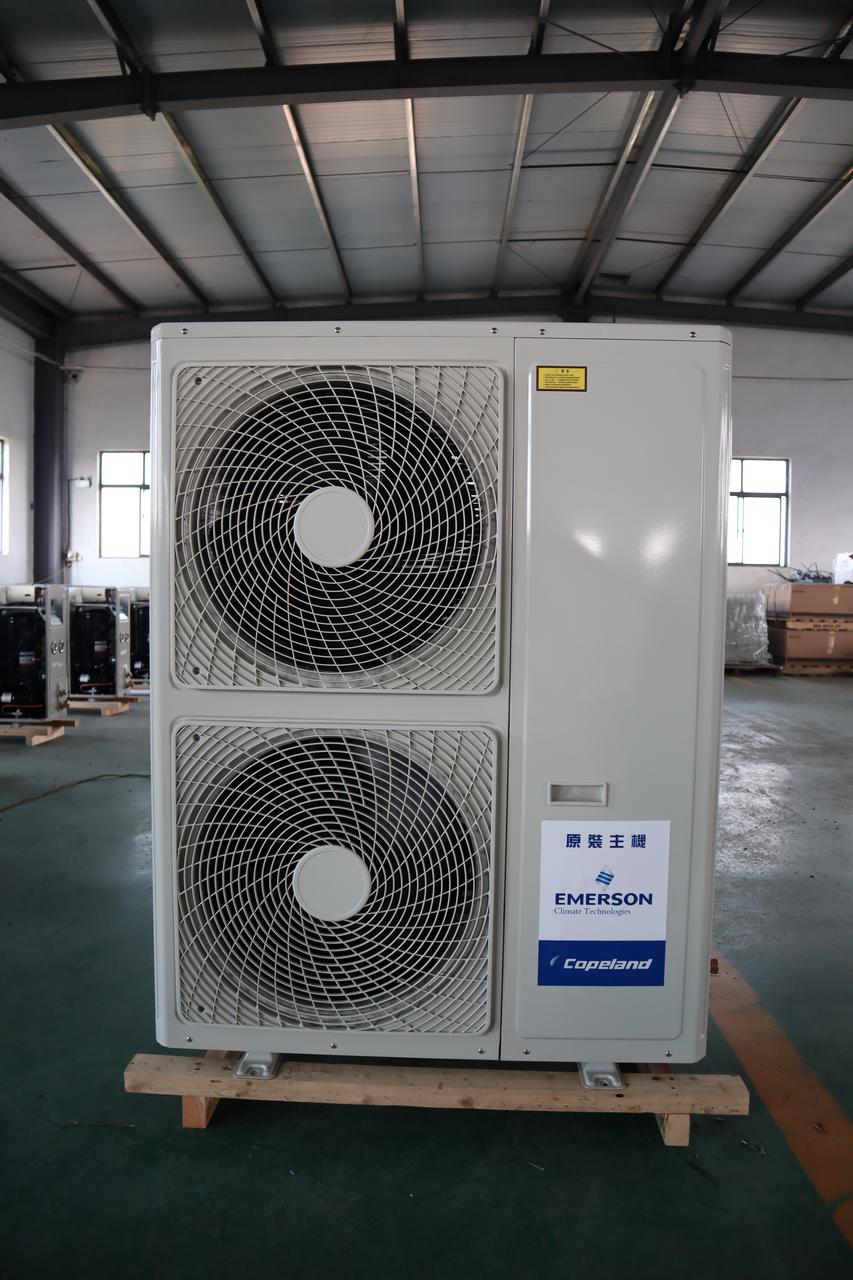
Professional pharmaceutical-grade condensingunits support precise temperature control within ±0.5°C, adapting to long-term uninterrupted operation. In line with industry compliance requirements, they adopt a one-main-one-standby dual-unit redundant configuration, matching an independent UPS emergency power supply system. The units can automatically switch in case of sudden power failure or unit failure, maintaining stable temperature in the cold room.
 |  |
3.Condensers: High-Efficiency Heat Exchange & Anti-Fouling Durable Adaptability
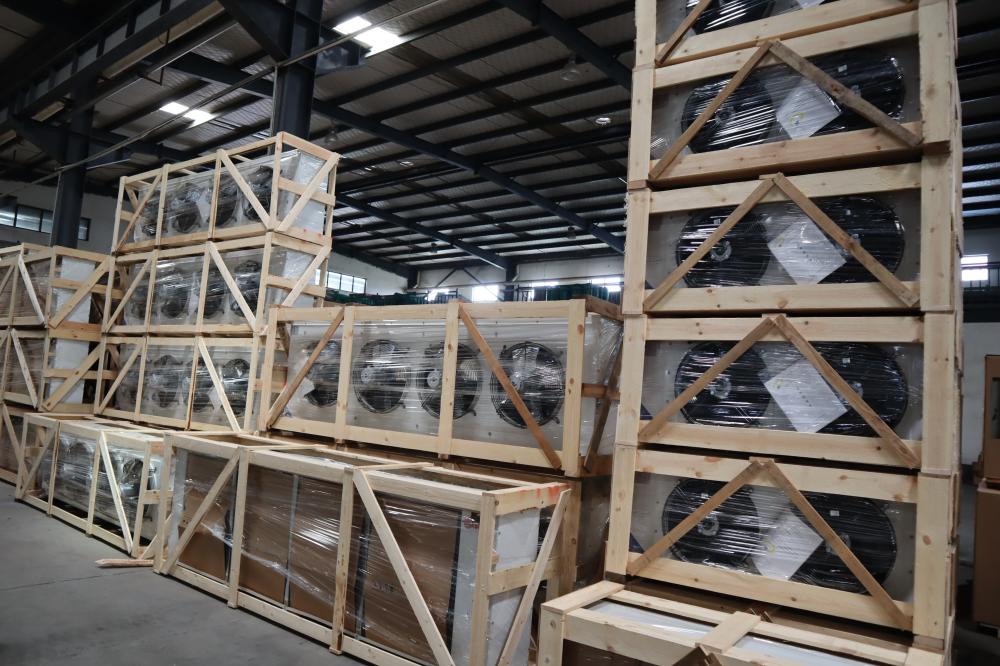
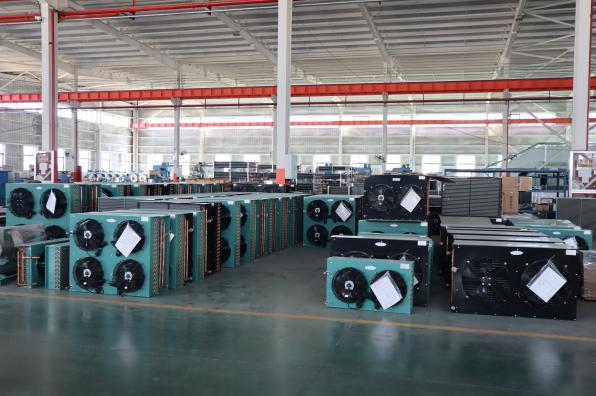
The stable heat exchange efficiency of condensers is the key to supporting the continuous and efficient operation of refrigeration units. Pharmaceutical cold chain scenarios put forward higher requirements for condenser heat dissipation efficiency and environmental adaptability. Ordinary condensers are prone to heat dissipation attenuation in high temperature, dust and other complex environments, resulting in increased unit load and temperature deviation.
Pharmaceutical special Condensers adopt optimized fin heat dissipation structure and high-precision heat exchange tubes, maintaining efficient and stable heat exchange rate in all weather conditions. Equipped with professional dust-proof and anti-corrosion coatings, they reduce the impact of external dust and humid environment on heat dissipation performance, effectively avoid unit overheating and frequent startup and shutdown problems. They ensure the refrigeration system always runs in a low-load and high-efficiency state, guaranteeing the long-term operational stability of pharmaceutical cold storage.
 |  |
Professional Customized Solutions & Service Support
Pharmaceutical cold chain cold storage construction is a systematic project integrating compliance, safety and stability. Unprofessional equipment matching will easily lead to failure in GSP acceptance, unstable cold room temperature, and high later-stage energy consumption. If you are preparing to build, renovate or upgrade pharmaceutical cold storage, please contact our YSHT professional technical team. We will combine your cold room scale, storage temperature zone and industry compliance standards, customize scientific and reasonable matching schemes forinsulation panels, Condensing Units and condensers for you, effectively control project costs, reduce later operation and maintenance risks, and provide full-process compliant and cost-effective cold chain equipment solutions for your pharmaceutical storage business.